AQL 2.5 does not mean that 2.5 percent of a shipment may be defective; it means a sampling plan that accepts a lot when defects in the drawn sample stay at or below a defined count. Under ISO 2859-1 at general inspection level II, a 1,200-piece order draws 80 pieces and passes with five or fewer minor-to-major defects, failing at six. A 3,200-piece lot draws 125 pieces and fails on the eighth. Fishing bag programmes normally run three classes at once: zero tolerance for critical faults, AQL 2.5 for major faults such as a failed weld or a split strap anchor, and AQL 4.0 for minor cosmetic issues. Knowing those numbers before writing the purchase order prevents the common argument about who pays for rework.
What an Acceptable Quality Limit Is, and What It Is Not
An acceptable quality limit is a statistical threshold used to decide whether to accept a lot from a random sample, and it is deliberately not a guarantee about the whole consignment. The plan is designed so that a lot sitting exactly at the agreed quality level is accepted about ninety-five percent of the time, which means there is a known producer risk of rejecting good goods and a known consumer risk of accepting a poor lot. Buyers who understand this stop treating inspection as a promise and start treating it as one cheap layer in a layered system.
The layered system is what actually delivers consistency. Layer one is incoming material verification, layer two is in-build checking at the operations that are expensive to redo, layer three is pre-shipment sampling, and layer four is retained-reference comparison for future disputes. Removing any layer increases the cost of the others; programmes that skip early checking reliably spend more on rework later.
Sample Size and Accept Numbers by Lot Size
The numbers below come from single sampling at general inspection level II under normal going, which is what most general merchandise inspection agreements specify. Read the row that matches the shipment size, draw that many pieces at random from across the packed cartons rather than from the top layer, and count each defect found. Switching to tightened checking after five consecutive passed lots is normal practice when problems appear.
| Lot size, pieces | Sample code | Pieces to inspect | Accept at AQL 2.5 | Reject at |
|---|---|---|---|---|
| 151 to 280 | G | 32 | 2 defects | 3 |
| 281 to 500 | H | 50 | 3 defects | 4 |
| 501 to 1,200 | J | 80 | 5 defects | 6 |
| 1,201 to 3,200 | K | 125 | 7 defects | 8 |
| 3,201 to 10,000 | L | 200 | 10 defects | 11 |
| 10,001 to 35,000 | M | 315 | 14 defects | 15 |
Random drawing is where plans quietly fail. All eight cartons cannot come from one pallet, and twenty pieces pulled from one carton are not twenty independent samples; inspectors should draw from at least the square root of the total carton count, spread across pallet positions. Most inspection providers build this into the standard protocol, but it is worth stating explicitly when writing an agreement.
Defect Classes: Critical, Major and Minor
Everything hinges on how findings are classified, because the same physical fault can pass or fail a lot depending on which column it lands in. A scratch inside a hidden seam is a minor finding; the same length scratch running through a load-bearing weld is a major one. Write the classification into the inspection agreement with examples, since this is the single most argued point between buyers and inspection teams.
| Class | Definition for fishing bags | Tolerance | Typical examples |
|---|---|---|---|
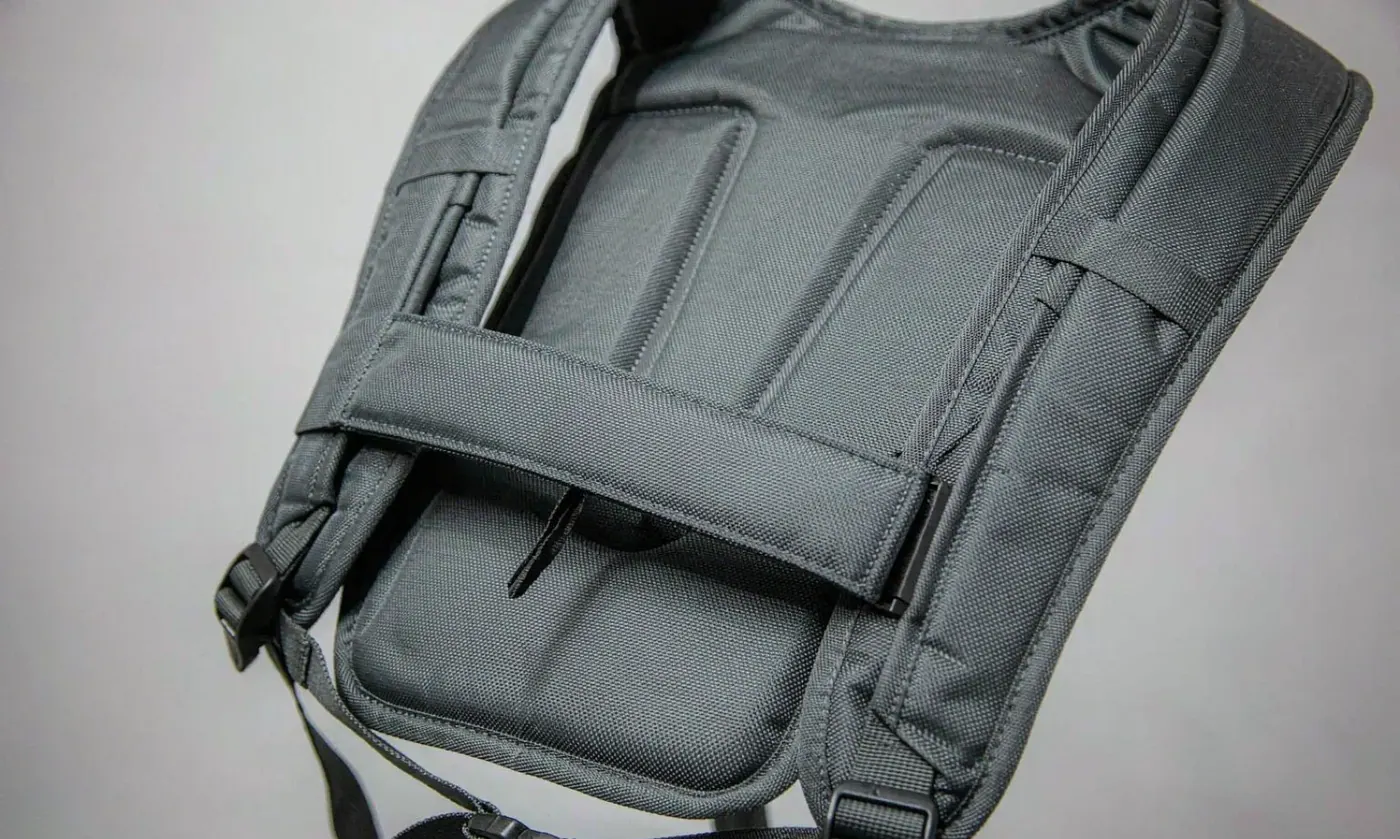
| Critical | Unsafe or unusable, or non-compliant with regulation | Zero tolerance | Needle left in padding, restricted substance breach, broken load strap |
| Major | Affects function or saleability for a reasonable buyer | AQL 2.5 | Split welded seam, open tray divider, zip that jams, missing logo |
| Minor | Cosmetic and small, unlikely to affect first use | AQL 4.0 | Thread ends over 5 mm, light creasing, small print misalignment |
| Observation | Not yet a defect, worth recording | No effect on result | Slight colour variation within an accepted range |
Note how few findings are genuinely critical and how many get argued into the major column. The useful discipline is to ask a simple question of each finding: would a retail customer notice this in the first ten minutes of ownership, and would they return the item for it? If yes to both, it is major. If they would notice but still keep the item, it is minor.
The Fishing Bag Check List Worth Writing Down
Generic handbag checks miss the faults that matter on a tackle bag, because a tackle bag carries eight kilograms of hard objects and gets wet every trip. The list below has caught more problems than any laboratory patch test, and each item takes under a minute per unit.
- Pull each strap anchor by hand and then, on two units per batch, hang fifteen kilograms for two minutes; look for stitch movement rather than for breakage.
- Cycle every zip twenty times and check that the slider travels without a catch; then look along the tape for pinholes at the fold.
- Press the base onto a flat surface and confirm the bag sits square; a rocking empty bag means the moulded base is distorted.
- Seat the stated number of trays and check that they slide without forcing; a tight cavity shows an internal dimension drift.
- Rub any print with adhesive tape once; a print that lifts at the edge will crack by the third month of use.
- Smell the interior. Residual solvent odour signals insufficient curing time before packing, which then transfers to retail packaging.
Dimension checking deserves its own line. Standard practice allows tolerance of plus or minus five millimetres on soft goods up to 600 millimetres, and about one percent beyond that, but the tolerance that actually matters commercially is internal: tray cavity width, because a cavity three millimetres under specification will not accept the tray sizes the marketing claims.
Where Checking Happens in the Build Sequence
Timing changes what inspection is worth. Material verification before cutting catches the expensive problems at the point where they cost least. Checking during the build catches parameter drift at the operations that cannot economically be undone. End-of-run random sampling is what produces the certificate, and container loading supervision is what makes sure what was inspected is what actually shipped.
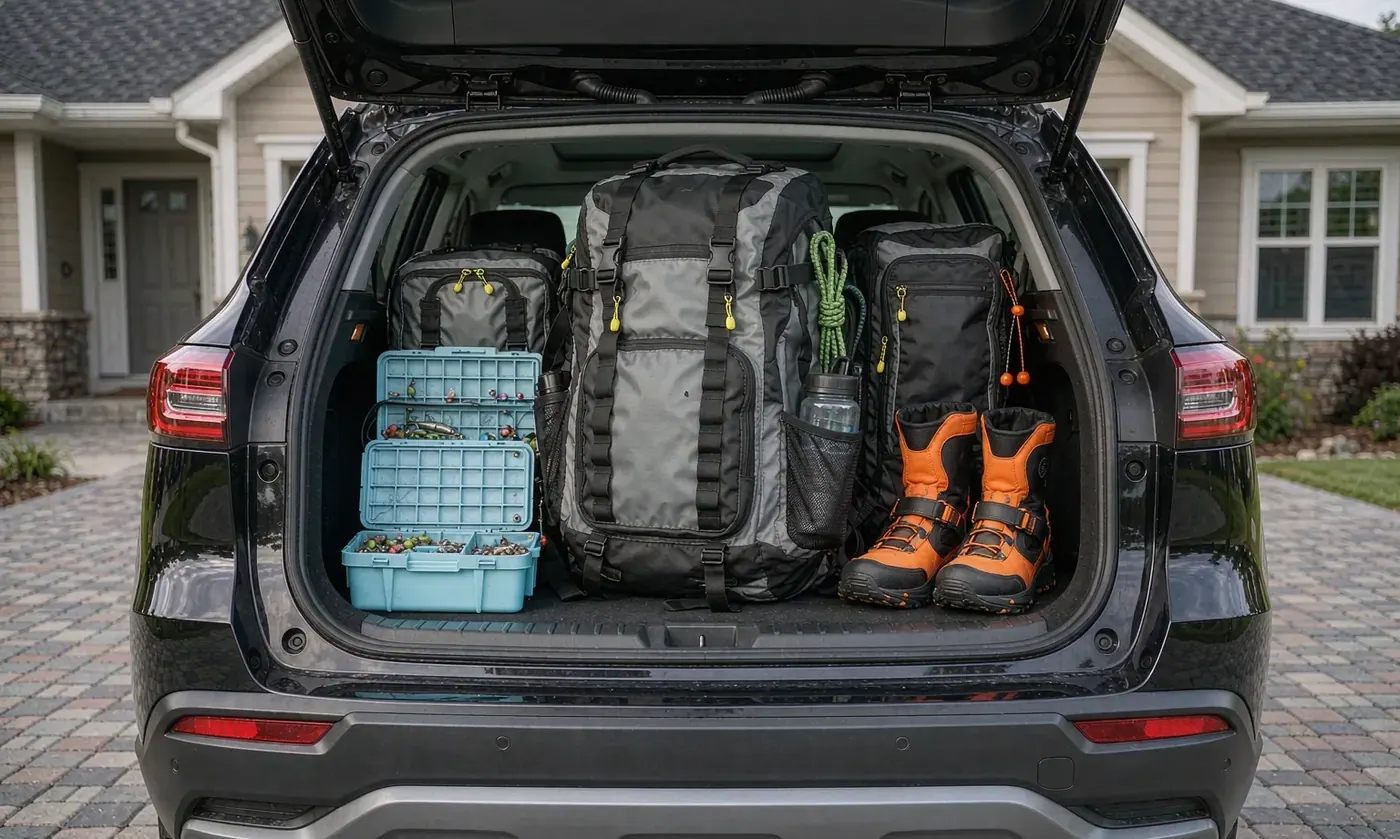
A practical sequence for a first order runs: material certificates and swatch comparison at booking, pilot-run review of the first thirty pieces with both parties present, mid-run review at roughly forty percent completion, then final sampling against the agreed plan. First orders need all four; repeat programmes with stable history can often drop to the pilot review and final sampling, which halves inspection cost without materially changing the outcome.
Typical Failure Distribution on Waterproof Builds
Distribution matters more than totals, because knowing which faults dominate lets a programme target an inspection list rather than reinspect everything at equal depth. Figures below describe the pattern commonly seen across general waterproof soft goods programmes and are meant as a starting allocation of attention rather than as a fixed measure.
| Fault group | Share of recorded findings | Detected at | Usual cause |
|---|---|---|---|
| Stitching and thread faults | 30 to 35 percent | Mid and final inspection | Needle heat, thread tension drift, blunt needles |
| Closure problems, zip and buckle | 20 to 25 percent | Final inspection | Hardware lot change, slider gauge mismatch |
| Cosmetic soiling and creasing | 15 to 20 percent | Final inspection | Handling without gloves, packing too early |
| Weld and seam tape faults | 10 to 15 percent | Pilot and mid run | Parameter drift after material lot change |
| Dimension drift | 5 to 10 percent | Pilot run | Pattern stretch on coated fabric |
The most useful observation from this distribution is that the two largest groups are both cheap to influence. Thread faults respond to a needle-change policy every four hours rather than at breakage, and hardware problems almost always trace to a component lot changed without the buyer being told, which is why no-substitution clauses matter more than tighter sampling.
A worked example makes the economics concrete. A 2,000-piece tackle backpack programme at twenty-two dollars unit value carries goods worth forty-four thousand dollars; inspection at two person-days plus travel typically lands between three and five hundred dollars, comfortably under one percent. Compare that with discovering the same fault after receipt: air-freighted replacement stock, discounted clearance of the affected units, and in a bad case a listing suspension lasting weeks. The honest conclusion is not that inspection guarantees quality, but that it is the cheapest available information about a shipment.
Cost, Who Pays, and What Re-inspection Involves
Third-party inspection is normally quoted per person-day, with one person-day covering roughly two to four lots depending on size and check-list depth. For a 2,000-piece fishing bag programme that typically lands under one percent of goods value, which is modest against the alternative. Many buyers also require the re-inspection costs to fall to the party whose goods failed, and that single clause does more to concentrate attention than any numerical threshold.
When a lot fails, three options exist and the sensible response depends on the finding. A widespread cosmetic issue can often be corrected by sorting and reworking, followed by a re-inspection at the failing partys cost. A functional fault affecting a measurable share of units usually means full lot rework. A safety or compliance finding means the lot does not ship, and the conversation moves to replacement rather than repair. Agreeing these outcomes in advance removes the negotiation when there is no time for one.
Documentation to Keep After Every Shipment
Records are what turn inspection into precedent. Keep the report together with the carton list, the retained sealed reference piece, and photographs of any defect found, and store them against the purchase order number. Six months later, when a retailer raises a quality issue on a repeat line, having the first shipment record to hand is usually enough to settle whether anything has actually changed.
Two habits add disproportionate value. Photograph the packing method as well as the product, because transit damage claims are resolved with those images. Retain one sealed sample per colour per season rather than per programme, since colour lots drift more than tools do. Finally, file the report under both the purchase order number and the design code, because most people search for one and most disputes refer to the other.
One more pairing is worth writing into every agreement because it prevents a specific and recurring argument: what counts as one defect. A single unit with three separate findings counts as three defects in most plans, which surprises buyers who expect each piece to count once. Stating that explicitly, together with whether a finding repeated across units of the same type counts as one cause or many instances, removes ambiguity when the result is borderline and the shipment needs to sail.
Why Not Simply Check Every Piece
The obvious answer to quality anxiety is to inspect the whole lot, and on occasion that is the right call, usually immediately after a failure when nothing is trusted. As a standing policy it performs worse than sampling, and for a reason that surprises buyers: inspection fatigue. A person checking eight hundred identical units finds fewer faults per hundred than a person checking eighty, because attention decays well before the workload does, and the faults that survive are precisely the intermittent ones that matter.
There is also a physical limit. Some critical checks are destructive or near-destructive: a sustained strap pull and a full zip cycle count cannot both be done on every unit without ageing the product before delivery. Sampling accepts a known residual risk in exchange for checks that are actually performed properly, and then reduces that residual risk through earlier checks in the build rather than through brute force at the end.
Packing, Carton Spine and Transit Damage
A meaningful share of retail complaints attributed to product quality are actually transit events. Cartons stacked eight high for six weeks compress the bottom layer, and individually bagged units in a loose master carton develop creases that no amount of inspection prevented. Two specifications remove most of this: a master carton rated to the stacking height it will actually see, with burst strength stated in kilopascals rather than described as strong, and internal fill that prevents movement rather than merely covering the top layer.
Transit testing is cheap insurance on a first programme and takes one afternoon. A drop test from the heights used in standard parcel handling, plus twenty-four hours under the weight of eight filled cartons, reveals whether the packing specification survives distribution. Where timelines allow, ship two cartons by the intended route before the bulk and open them: for roughly the price of express freight, the whole distribution assumption is validated or corrected while there is still time.
Switching Rules Every Buyer Should Know
Inspection plans are not static; the standard expects them to move with demonstrated history. Under normal checking, two out of five consecutive lots failing moves the programme to tightened checking, which usually means moving to the next larger sample size with the same accept numbers, so statistically harder to pass. Coming back off tightened status requires five consecutive accepted lots, which is deliberately slow. Conversely, ten consecutive accepted lots under normal checking can qualify a mature programme for reduced checking, cutting sample sizes by roughly a third and with them the inspection bill.
Buyers benefit from knowing this because it changes the conversation with a partner whose numbers were poor last quarter. The way back is mechanical and takes five clean shipments, so there is little value in arguing about any single borderline result. Programmes that understand switching rules also tend to write better disagreements into their agreements: rather than threatening to reject everything after one questionable lot, they can state that two failures within five consecutive shipments trigger tightened checking at the other partys cost.
Corrective Actions That Actually Stick
Every programme eventually finds a fault worth fixing, and most responses fail because they ask people to try harder rather than changing something physical. Thread faults from heat-blunted needles are solved by a scheduled four-hour needle change, not by reminding operators. Hardware problems from undocumented substitution are solved by a change-control clause with a named consequence, not by another email. Recurrence comes from treating the root cause as a policy rather than as a mechanism.
Write corrective actions so they can be verified by someone who was not present. The action should name the physical change, the person responsible, the date it takes effect, and the evidence that will exist afterwards, such as a needle-change log or a revised carton specification. Vague follow-up produces vague improvement and the same finding appears two shipments later, which is usually the point at which a commercial relationship starts to strain.
Programme Notes and How the Acceptance Standard Is Written
QUANZHOU JUNYUAN BAGS has run waterproof bag programmes since 2014 with a founding team in this trade since 2004, inspecting every bulk shipment at AQL 2.5 before release and retaining sealed reference pieces for each colourway. Programmes operate under BSCI and ISO 9001 governance, with incoming materials screened for REACH and California Prop 65 and monthly output running at 200,000 units verified by SGS. Opening orders begin at 500 pieces per design and colour, sampling takes six to ten working days, and bulk production takes thirty-five to fifty days from approved sample and deposit.
The acceptance plan itself is best written once and reused. Cite sampling tables and switching rules from the International Organization for Standardization, name the physical methods to be used such as strap pull and coating adhesion from ASTM International, and keep chemical expectations separate from mechanical ones by referring to the material documentation described in the REACH and Prop 65 material guide. Order economics are set out in the MOQ guidance for fishing bag orders, and seam expectations in the radio frequency welding process notes. Briefs go to service@junyuanbags.com.
People Also Ask
How many pieces are checked for a 1,000-piece fishing bag order?
Eighty pieces drawn at random, under ISO 2859-1 general inspection level II. The lot passes with five or fewer defects and fails at six.
Is AQL 2.5 the same as allowing 2.5 percent defects?
No. It is a statistical sampling threshold, not a permitted defect rate for the whole shipment, and lots at the limit are accepted about ninety-five percent of the time.
What is a critical defect on a tackle bag?
Anything unsafe, unusable or non-compliant, such as a needle retained in padding, a restricted substance breach, or a load strap that fails under fifteen kilograms.
What is the difference between AQL 2.5 and AQL 4.0?
AQL 2.5 applies to major faults affecting function or saleability; AQL 4.0 is the looser band used for minor cosmetic findings that would not trigger a return.
Who pays for re-inspection when a lot fails?
Usually whoever is responsible for the failure, provided the purchase order states it. Without that clause the cost defaults to whoever is asking for the check.
Should every order be fully inspected?
Not economically. At these quantities, random sampling plus early build checks gives better value than hundred percent inspection, except where a safety issue is suspected.
Frequently Asked Questions
Q1. What does AQL 2.5 mean in plain terms?
A defined count of allowable defects in a random sample. For a lot of 501 to 1,200 pieces, eighty are drawn and the shipment passes with five or fewer defects.
Q2. Which defects count as major on a fishing bag?
Faults affecting function or saleability: a split welded seam, a jammed zip, a missing tray divider, a distorted base, or a missing logo.
Q3. How common is a failed result when the plan is followed?
Rare on stable programmes with no material changes. Failures cluster on first production runs and after any trim or hardware substitution.
Q4. Can an inspection be done during loading only?
It can, but it shifts everything to the last moment. A pilot review of the first thirty pieces catches parameter drift while it can still be corrected economically.
Q5. How many cartons should the sample come from?
Draw from at least the square root of the total carton count, spread across pallet positions, rather than pulling units from one convenient carton.
Q6. What tolerance applies to bag dimensions?
Around plus or minus five millimetres on pieces up to 600 millimetres, and about one percent beyond that, though internal tray cavity width usually matters more.
Q7. Should straps be pull-tested on every unit?
No. Sample two units per batch with a static fifteen kilogram load for two minutes and inspect the rest visually for stitch movement at the anchor.
Q8. How long should inspection records be kept?
At least through the following selling season, and ideally for the full liability period, since they settle whether a repeat line has genuinely changed.
Q9. What is tightened inspection?
A switch to a stricter plan triggered when five consecutive lots show problems. It stays in force until quality stabilises and normal switching conditions return.
Q10. Does every order include a sealed reference sample?
It should. Retaining one sealed piece per colourway per season settles disputes about whether a repeat line has genuinely changed far faster than photographs alone.
Q11. Does a higher acceptance standard raise unit cost?
Only modestly. Tightening from AQL 2.5 to AQL 1.0 increases sorting and rework effort, typically adding around one to three percent to unit cost.